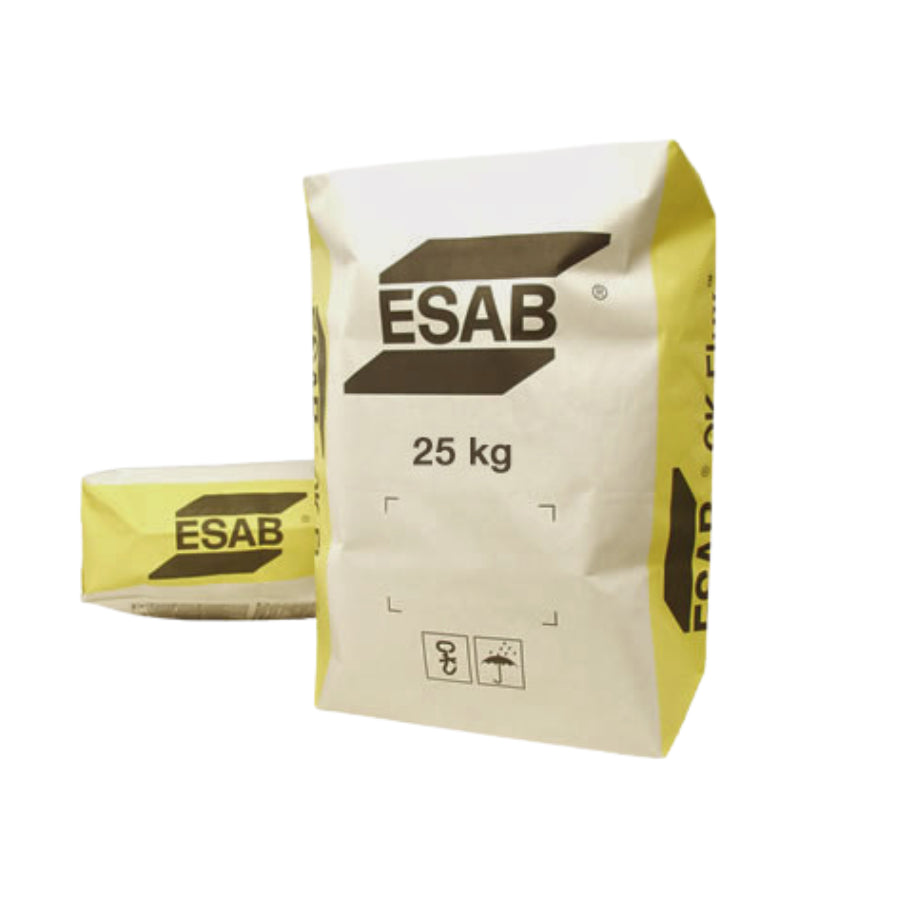

SAW Powder ESAB OK Flux 10.71 25 kg Bag
Delivery time: 7-10 days
Couldn't load pickup availability
Discover suitable special offers and accessories for your welding setup.
ESAB OK Flux 10.71 – Neutral SAW flux for multi-pass welding
- 25 kg bag
- Item no. 1071000200
The ESAB OK Flux 10.71 is a neutral, bonded (agglomerated) welding flux for submerged arc welding (SAW) of non-alloyed and low-alloyed steels. It is primarily designed for multi-pass butt and fillet welds and offers very high process stability in automated welding applications.
The flux is suitable for AC and DC operation, single and multi-wire systems, and current intensities up to 1000 A. It is characterized by stable arc guidance, uniform penetration, and easy slag removal.
Not recommended for applications with heavily rusted or heavily scaled base materials.
Typical application areas
- Steel and plant construction
- Bridge construction
- Heavy machinery and vehicle construction
- Pipe and linepipe production
- General structural and construction welding
Product features
- Neutral, bonded (agglomerated) SAW flux
- Very good arc stability
- Uniform penetration
- Very good slag removal
- Suitable for multi-pass welding
- Single and multi-wire operation possible
- Designed for high current intensities up to 1000 A
Technical data
| Welding process | Submerged arc welding (SAW) |
| Flux type | Bonded (agglomerated) |
| Chemical character | Neutral |
| Slag type | Aluminate-basic |
| Suitable materials | Non-alloyed and low-alloyed steels |
| Current type | AC / DC |
| Wire systems | Single and multi-wire |
| Max. current | up to 1000 A |
| Diffusible hydrogen | max. 5 ml / 100 g weld metal (dried flux) |
| Density | approx. 1.2 kg/dm³ |
| Basicity index | approx. 1.5 |
| Alloy transfer | Slight silicon, moderate manganese alloying |
Standards & Classifications
AWS A5.17
- F7P5-EH12K
- F7P4-EM14K
- F7A5-EH12K
- F7A4-EM13K
- F7A4-EM12K
- F7A2-EM14K
AWS A5.23
- F8A4-ENi1K-Ni1
- F8A2-EA2-A4
- F7P0-EA2-A4
Approvals
- CWB (AWS A5.23 / CSA W48)
- DB (Deutsche Bahn)
- NAKS / HAKC
- CE according to EN 13479
Note: Approvals depend on the manufacturing plant.
Typical wire combinations
- OK Autrod 12.24
- Spoolarc 29S
- Spoolarc 53
- Spoolarc 71
- Spoolarc 75
- Spoolarc 81
The mechanical properties of the weld metal (e.g., yield strength, tensile strength, notch impact energy) result from the specific combination of flux and welding wire.
Product safety information
ESAB
Welding Technology
ESAB Welding & Cutting GmbH
Langenfeld branch
Winkelsweg 178 – 180
40764 Langenfeld
Germany
Phone: +49 2173 3945-0
E-mail: info@esab.de
Or
Cutting Technology
ESAB Welding & Cutting GmbH
Robert-Bosch-Str. 20
61184 Karben
Germany
Phone: +49 6039 40-0
E-mail: info@esab.de, info@esab-cutting.de
Product safety and documents
Manufacturer
Product identification
- SAW flux ESAB OK Flux 10.71 25 kg bag · Item no. 1071000200 · EAN 1071000200
Technical Data
Technical Data
Product details
Product details
Choose welding technology based on material, process, performance, and location. For questions regarding accessories, wear parts, or alternatives, we are happy to help.
Notes & Application
Notes & Application
Before use, observe the operating instructions, protective measures, and manufacturer's specifications. Use suitable consumables and regularly check wear parts.
Your payment information will be processed securely. Depending on the shop settings, several payment methods are available.