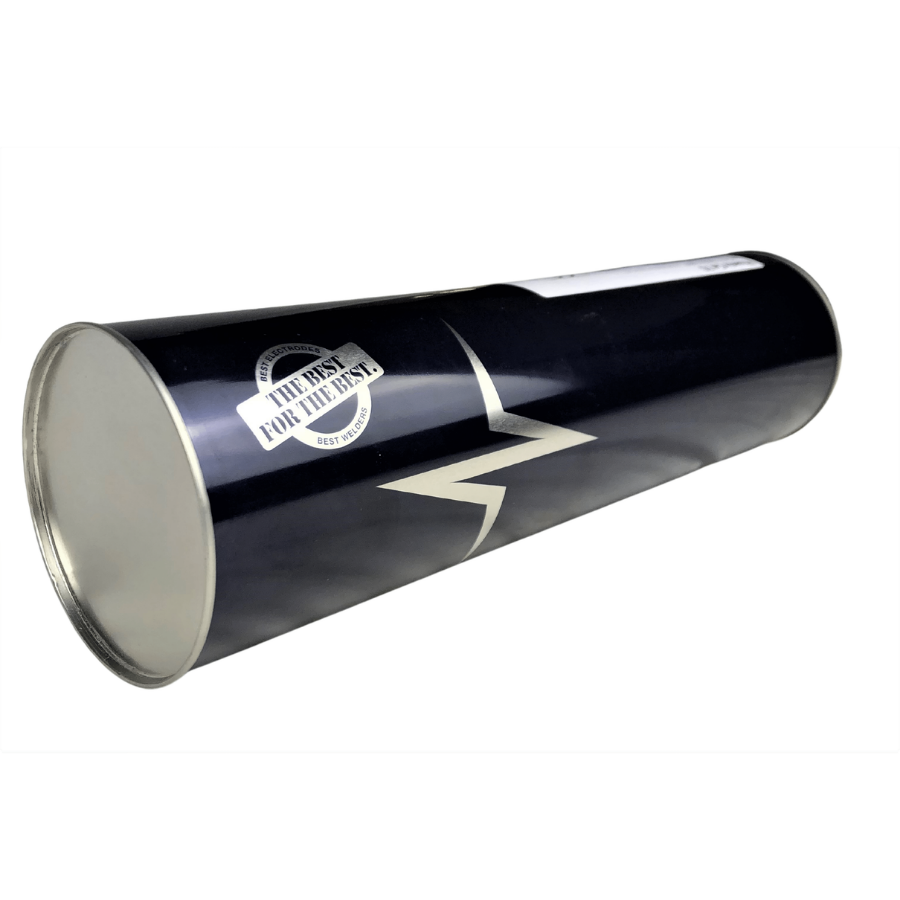

Stick Electrodes Böhler FOX DCMS KB
Available in stock (15)
Lieferzeit: 1-2 Tage
Couldn't load pickup availability
Discover suitable special offers and accessories for your welding setup.
Stick Electrodes Böhler FOX DCMS KB
- Basic coated stick electrode Böhler FOX DCMS KB
- Heat resistant up to 570°C
- Weld metal of type 1Cr-0.5Mo
- Pleasant weldability
- Yield of 115%.
| Standard designation | |||
| EN ISO 3580-A | EN ISO 3580-B | EN ISO 2560-A | EN ISO 2560-B |
| E CrMo1 B 4 2 H5 | E5518-1CM H5 | E5518-B2 H4 | E8018-B2 H4 |
Description:
The BÖHLER FOX DCMS kb is a stick electrode with an alloyed core and a basic coating. The weld metal of this electrode, which corresponds to type 1Cr-0.5Mo, is characterized by a bainitic microstructure. It is suitable for various applications, both in the tempered state and after quenching and tempering, and under certain conditions even in the as-welded state. This product is particularly suitable for joining similar heat-resistant steels and cast steels in plants and vessels used in power plant construction and the chemical industry. The BÖHLER FOX DCMS kb is approved for long-term use at temperatures up to 570 ºC.
The weld metal contains only very small amounts of accompanying and trace elements, resulting in a typical Bruscato factor of less than 12. This electrode is resistant to temper embrittlement and reliably meets the requirements of the step-cooling test conditions. The basic coating of the stick electrode ensures a low content of diffusible hydrogen in the weld metal and a weld metal recovery of 115%.
Base materials for Böhler FOX DCMS KB
similar heat-resistant steels and cast steel 1.7335 13CrMo4-5, 1.7262 15CrMo5, 1.7728 16CrMoV4, 1.7218 25CrMo4, 1.7225 42CrMo4, 1.7258 24CrMo5, 1.7354 G22CrMo5-4, 1.7357 G17CrMo5-5 ASTM A 182 Gr. F12; A 193 Gr. B7; A 213 Gr. T12; A 217 Gr. WC6; A 234 Gr. WP11; A335 Gr. P11, P12; A 336 Gr. F11, F12; A 426 Gr. CP12
Special Notes
The required preheating, interpass temperature, and post-weld heat treatment parameters should be determined according to the properties of the respective base material. As a rough guideline, preheating in the range of 200 to 300ºC can be recommended, with the exact temperature possibly depending on the workpiece thickness. Typical temperatures for post-weld heat treatment are in the range of 600-700ºC.
Approvals of Böhler DCMS KB:
TÜV (0728), DB (10.014.42), ABS, DNV, NAKS ( Ø 3.2 mm; Ø 4.0 mm), CE
Technical Data
Technical Data
Product details
Product details
Choose welding technology based on material, process, performance, and location. For questions regarding accessories, wear parts, or alternatives, we are happy to help.
Notes & Application
Notes & Application
Before use, observe the operating instructions, protective measures, and manufacturer's specifications. Use suitable consumables and regularly check wear parts.
Your payment information will be processed securely. Depending on the shop settings, several payment methods are available.