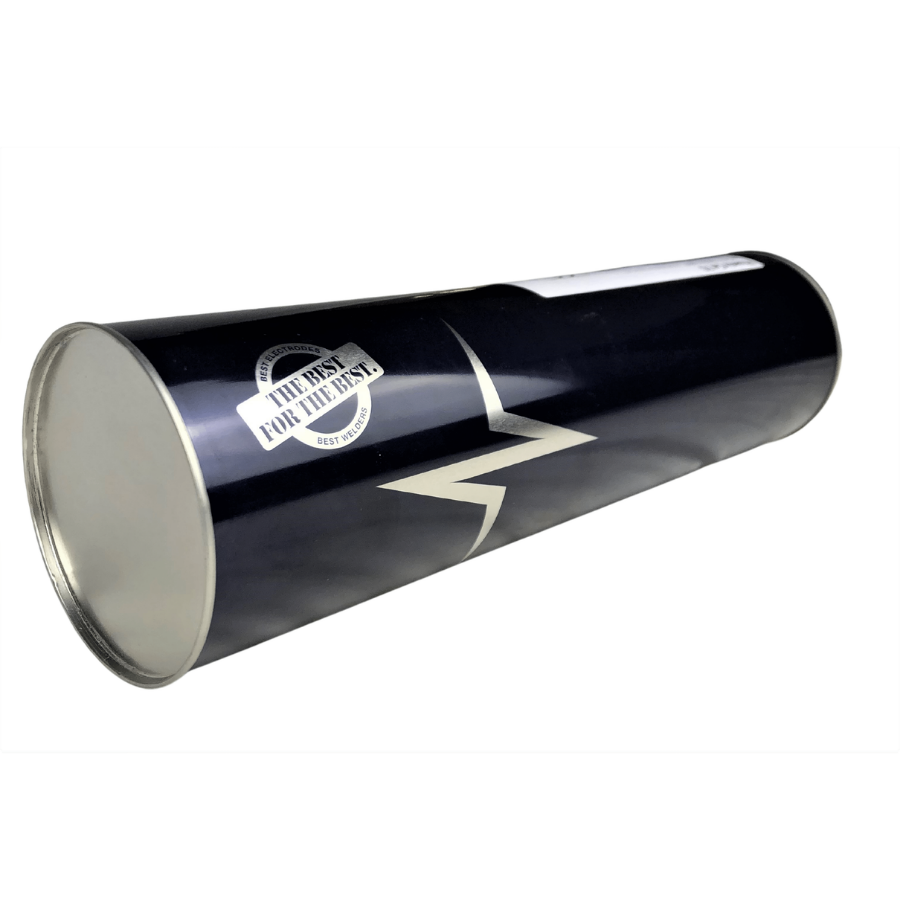

Stick Electrodes Böhler FOX A 7-A
Lieferzeit: 7-10 Tage
Couldn't load pickup availability
Discover suitable special offers and accessories for your welding setup.
Böhler FOX A 7-A Stick Electrodes
- Rutile-basic coated stick electrode
- For "black-white" joints
- Suitable for DC and AC current
- Suitable for buffer and intermediate layers
- Type E Z 18 9 MnMo R / E307 -16
| Standard designation | |
| EN ISO 3581-A | AWS A5.4 / SFA-5.4 |
| E Z 18 9 MnMo R 3 2 | E307-16 (mod.) |
Description:
This core wire alloyed stick electrode, type E Z 18 9 MnMo R / E307 -16, has a rutile-basic coating and is suitable for various welding applications, both for joining and surfacing in all positions except vertical-down. It is ideal for "black-white" joints, less weldable steels, austenitic manganese work-hardening steels, and repair work. The electrode is also suitable for buffer and intermediate layers on rails and switches, valve seats, and in hydropower plants.
The welds are characterized by cold-work hardening capability, high cavitation resistance, crack resistance, resistance to thermal shock, and scale resistance up to 850 °C. They are also largely insensitive to embrittlement by sigma phases above 500 °C. Post-weld heat treatment can be performed. For operating temperatures above 650 °C, it is advisable to consult our application technology department. The arc is stable with both DC and AC current. The ferrite content according to WRC 92 is 4–8 FN.
Base Materials for Böhler FOX A 7-A
This electrode is suitable for mixed joints between different types of steel, including structural steels, fine-grain structural steels, and quenched and tempered steels, which are joined with high-alloy chromium and chromium-nickel (molybdenum) steels. It is also suitable for joints between structural, quenched and tempered, and armored steels, as well as between unalloyed or alloyed boiler or structural steels and high-alloy chromium and chromium-nickel steels. Furthermore, it can be used for heat-resistant steels up to 850 °C and for joints between austenitic manganese work-hardening steels and other steels. This electrode is also ideal for joining cryogenic sheet and pipe steels with cryogenic austenitic materials.
Notes:
Preheating and interpass temperature must be adjusted to the base material.
Re-drying: if necessary, 250-300ºC, min. 2 hours. Removal from the can or Drysystem, in exceptional cases.
Approvals:
TÜV (02078), DB (30.014.40), CE
Product Safety Information
Böhler
voestalpine Böhler Welding Group GmbH
Peter-Müller-Straße 14-14a
40468 Düsseldorf
Phone: +49 (0) 211 580660-0
Email: welding@voestalpine.com
https://www.voestalpine.com/highperformancemetals/deutschland/de/
Technical Data
Technical Data
Product details
Product details
Choose welding technology based on material, process, performance, and location. For questions regarding accessories, wear parts, or alternatives, we are happy to help.
Notes & Application
Notes & Application
Before use, observe the operating instructions, protective measures, and manufacturer's specifications. Use suitable consumables and regularly check wear parts.
Your payment information will be processed securely. Depending on the shop settings, several payment methods are available.